 Skip to main content Skip to footer
A packaging logo can look sharp on a screen but lose clarity once it reaches a printed box. Small details, incorrect color settings, unsuitable artwork files, or poor placement can cause blurred edges, color shifts, and inconsistent results across different packaging runs. These problems become more costly when they appear after sampling or during mass production.
A print-ready packaging logo should combine strong visual design with practical production requirements. This guide explains the key design, color, material, printing, finishing, placement, and artwork decisions that help you achieve clear and consistent logo reproduction on custom boxes.
What Makes a Logo Suitable for Packaging Printing?

A logo is suitable for packaging printing when it stays clear, legible, and consistent on the finished box. Materials, scale, printing methods, and finishes can all change how a logo looks, so the design must reproduce well beyond the screen.
- Clear structure: Simple shapes and defined edges reproduce more accurately across different printing processes.
- Strong legibility: Text and graphic elements remain easy to recognize at the intended print size.
- Good contrast: The logo stands out clearly from the paper color, texture, or printed background.
- Scalability: The design remains recognizable across small cartons, rigid boxes, and larger packaging formats.
- Print compatibility: The artwork can adapt to ink printing, foil stamping, embossing, and other finishing methods without losing key details.
- Consistent reproduction: The logo maintains a similar appearance across different box materials, SKUs, and repeat production runs.
Design Packaging Logo Details That Reproduce Clearly

Packaging logo details should be designed for clear reproduction without losing the brand’s visual character. Fine strokes, tight spacing, small gaps, and overly intricate graphics can lose definition during printing or finishing. Each element should remain distinct and recognizable at the final print size and suit the selected production method.
- Typography: Use letterforms that remain readable after printing. Extremely thin strokes, tight spacing, and very small counters can fill in or lose definition.
- Graphic elements: Keep icons, symbols, and illustrations distinct enough to remain recognizable when reproduced on packaging.
- Line weight: Avoid hairline strokes that may disappear or print unevenly. Important outlines should have enough thickness for the selected production process.
- Negative space: Leave sufficient space between letters, shapes, and graphic elements so they do not merge when ink spreads slightly or finishing tolerances vary.
- Design complexity: Reduce unnecessary details that only work at large digital sizes. A simplified version often performs better for small packaging applications.
- Gradients and transparency: Use these effects carefully because some printing and finishing processes reproduce them less predictably than solid shapes.
- Logo variations: Prepare simplified or single-color versions when the primary logo contains details that cannot transfer cleanly to every packaging application.
Choose the Right Color System for Packaging Logo Printing
The right color system helps your packaging logo reproduce more accurately from artwork to the finished box. RGB works for screens, while printed packaging usually relies on CMYK or Pantone spot colors. Your choice depends on the logo design, required color accuracy, printing method, and production volume.
RGB and CMYK Color Modes

RGB is designed for digital screens, while CMYK is the standard color model for most process-color packaging printing. RGB creates color with red, green, and blue light, whereas CMYK builds printed color with cyan, magenta, yellow, and black inks. Because the two systems use different color gamuts, highly saturated RGB colors, especially neon-like shades, often become more muted after conversion to CMYK.
For packaging projects, designers should convert artwork to CMYK early enough to review these shifts before sampling or production. CMYK works well for multi-color logos, gradients, photographs, and complex graphics, but it does not make color completely predictable by itself. Paper tone, ink absorption, coatings, and printing conditions can still change the final appearance, so critical brand colors may require a separate spot-color reference.
Pantone Spot Colors
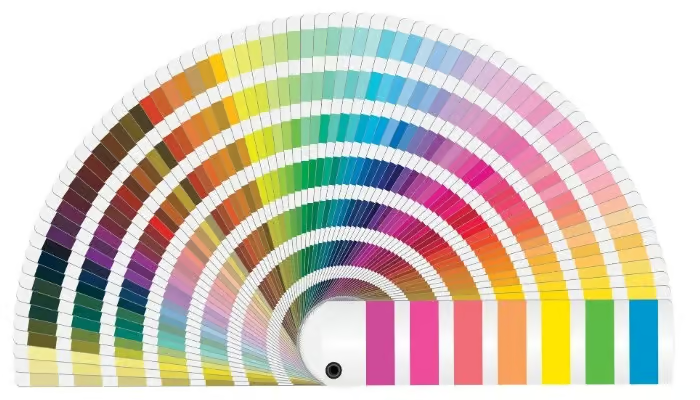
Pantone spot colors provide tighter control when a packaging logo depends on a specific brand shade. The Pantone Matching System uses standardized color references, and printers reproduce those colors with separately mixed inks rather than creating them only from overlapping CMYK dots.
Spot colors work particularly well for main logo marks, corporate typography, and one- or two-color branding where color accuracy matters more than full-color flexibility. They also give manufacturers and buyers a clearer reference for repeat orders and multi-SKU packaging programs. However, the same Pantone reference can still look slightly different on coated, uncoated, kraft, or colored papers, so physical samples remain important when the brand color is critical.
Adapt Your Packaging Logo to Different Box Materials
The same packaging logo can look different when it is printed on different paper surfaces. Paper color, coating, texture, and ink absorption all affect contrast, edge definition, and color appearance. You should therefore design the logo together with the actual box material instead of treating the artwork as an independent element.

Coated and Uncoated Paper
Coated paper supports sharper edges, stronger color density, and finer logo details because the surface absorbs less ink. Thin typography, detailed symbols, gradients, and multi-color logos usually reproduce with greater definition on smooth coated stock.
Uncoated paper absorbs more ink, which can soften edges and reduce color intensity. For logos used on uncoated boxes, you should avoid overly fine strokes, very small text, and narrow negative spaces. Slightly heavier lines and simpler details help the logo remain clear at the final print size.
Kraft and Colored Paper
Kraft and colored paper require stronger contrast because the paper color affects the visible result of the logo. Brown kraft can mute transparent inks, while dark paper can reduce the visibility of mid-tone brand colors.
You can improve clarity by using darker solid inks on light kraft, opaque white underprinting on dark substrates, or single-color logo versions with stronger contrast. Foil stamping and embossing also work well when the paper color already plays a strong role in the packaging design.
Textured and Specialty Paper
Textured and specialty papers need logo designs with stronger shapes and fewer delicate details. Uneven surfaces can interrupt fine lines, small lettering, and narrow gaps, which makes intricate artwork less consistent than it appears in the original file.
For these materials, use clearer contours, wider line weights, and sufficient spacing between elements. If the texture is pronounced, foil stamping, embossing, debossing, or screen printing can create a cleaner logo than fine conventional ink printing.
Size and Position Your Packaging Logo Correctly on the Box
Logo size and placement should support clear recognition without competing with the box structure or other design elements. The right scale, safe area, dieline position, and viewing direction help the logo stay visible, balanced, and consistent across different packaging formats.

Logo Size and Scale
For most custom boxes, a primary logo occupying about 20–35% of the usable panel width provides a practical starting point. A restrained luxury layout can reduce this to about 12–20%, while a logo-led design may increase it to 35–50%.
Once the logo approaches 50–60% of the usable panel width, it usually starts competing with margins, product information, or structural areas rather than functioning as a balanced brand mark. These percentages are layout guidelines rather than fixed printing standards because logo proportions and box formats vary.
The lower limit depends on the smallest element inside the logo. As a practical rule, keep small logo text around 6–8 pt or larger for conventional ink printing, and avoid shrinking a detailed wordmark below roughly 25–30 mm in width without checking a physical proof. Adobe notes that 6 pt is generally the smallest readable size for product-label text, which provides a useful lower reference for packaging artwork.
Safe Printing Areas
Keep the packaging logo inside a defined safe area rather than placing it close to trim lines, folds, or wrapped edges. A practical starting point is to use 3 mm bleed beyond the cut line and keep the logo or other critical elements at least 3–5 mm inside the trim line. Around folds, creases, lid edges, die-cut windows, or wrapped corners, increase the clearance to about 5–8 mm where the structure allows.
These values work as design starting points, not universal production tolerances. The final dieline should control the logo position, because box structure, board thickness, cutting, folding, and wrapping can change the required safe area.
Dielines and Box Structure
The dieline should guide logo placement according to the assembled box, not just the flat artwork. A logo can appear centered on the dieline but look visually off-center after the box is folded, wrapped, or assembled.
Different box structures create different placement rules. On a magnetic closure box, the lid usually becomes the main branding surface. On a drawer box, the logo can sit on the sleeve, drawer front, or both, but each position creates a different visual focus. For lid-and-base boxes, the visible lid area should define the logo position rather than the full flat panel.
You should also consider opening direction and panel orientation. A logo may appear upside down or sideways when the customer opens the box if the artwork follows the flat dieline without considering use. Always position the logo based on the finished box orientation, then use the dieline to transfer that position accurately into production artwork.
Primary Viewing Area
Place the primary logo on the face customers see first, such as the top lid of a gift box, the front panel of a retail carton, the sleeve face, or the drawer front. Keep the logo aligned with the finished viewing direction, and use the vertical center or upper third of the panel as a practical starting position when the layout allows.
A top-facing logo suits boxes opened from above, while a front-facing logo works better for shelf display. Surrounding product names, windows, patterns, and decorative elements should support the logo rather than compete with it.
Select a Suitable Printing Method for Packaging Logos
Different printing methods reproduce the same packaging logo in different ways. Fine details, color count, substrate type, ink coverage, and order volume all affect the result, so the best process depends on the actual logo artwork and box specification.
Offset Printing

Offset printing is a strong choice for medium- to high-volume premium box projects that require sharp logo edges, fine typography, and controlled brand colors. It reproduces detailed artwork cleanly and supports both CMYK process colors and Pantone spot inks, making it suitable for logos that need precise color targets.
The main trade-off is setup cost. Offset printing requires separate printing plates for each color and press setup before production begins, so it is less economical for very small runs. As order volume increases, however, the setup cost is spread across more boxes, making offset printing more practical for larger production quantities.
Digital Printing

Digital printing works well for short runs, prototypes, multiple SKUs, and packaging projects that need frequent artwork changes. It prints directly from the digital file without separate printing plates, which makes setup faster and allows different logo versions to move into production with less preparation.
Modern digital presses can reproduce fine text, gradients, and full-color logo artwork clearly, especially on smooth coated paper. You will commonly see it used for short-run folding cartons, prototype boxes, paper sleeves, personalized gift boxes, and small-batch rigid box wraps. The process also suits variable designs, regional versions, QR codes, and personalized packaging. For very large runs or projects that require tightly controlled spot colors, offset printing may still offer better cost efficiency and color consistency.
Screen Printing

Screen printing favors packaging logos with bold shapes, solid colors, and sufficient line weight. Because the ink passes through a mesh screen, very thin strokes, tiny text, and narrow gaps can lose definition or fill in during printing.
It is particularly useful for rigid boxes, kraft boxes, textured paper boxes, specialty paper-wrapped gift boxes, and other packaging surfaces where stronger ink coverage is needed. For a screen-printed logo, simplify intricate details, increase spacing between small elements, and avoid relying on smooth gradients or subtle tonal transitions. A strong one- or two-color logo with clear boundaries usually reproduces more consistently than a highly detailed mark.
Flexographic Printing

Flexographic printing reproduces simple packaging logos efficiently with solid colors, bold shapes, and clear outlines. The process uses flexible relief plates, so slight ink spread and plate pressure can soften very fine details compared with offset printing. It performs best with one- or two-color logos, larger text, and graphic elements that do not depend on delicate gradients or tight spacing.
Thin strokes, small counters, narrow negative spaces, and subtle tonal transitions may lose definition during printing. A flexographic logo therefore benefits from stronger line weight, wider spacing, and simplified vector artwork, especially when printed on corrugated board, kraft paper, or other absorbent packaging surfaces.
Gravure Printing

Gravure printing is more common for very high-volume packaging that uses continuous printed materials, including some folding cartons, laminated paper packaging, and specialty paper wraps. It can reproduce fine logo details, smooth gradients, and dense color areas with strong consistency across long production runs.
Logo artwork can include more complex tonal transitions than flexographic designs, but the final file still needs clean vector elements for wordmarks, symbols, and small text. Because gravure relies on engraved cylinders, it is generally better suited to standardized packaging designs that will run in large quantities rather than frequently changing logo versions.
Packaging Logo Printing Method Comparison
The table below compares the main printing methods by logo characteristics, suitable box types, and key design considerations. Use it as a quick reference to match your packaging logo with the most practical printing process before finalizing the artwork.
| Printing Method | Best Logo Characteristics | Suitable Packaging Types | Main Design Considerations |
| Offset Printing | Fine typography, detailed graphics, CMYK or Pantone colors | Rigid boxes, folding cartons | Supports fine details and gradients; define colors clearly |
| Digital Printing | Full-color logos, gradients, variable artwork | Short-run boxes, prototypes | Good for multiple SKUs and frequent artwork changes |
| Screen Printing | Bold shapes, solid colors, simple logos | Rigid boxes, kraft boxes | Avoid thin strokes, tiny text, and subtle gradients |
| Flexographic Printing | Simple vector logos, solid fills, strong outlines | Corrugated boxes, mailer boxes | Use wider spacing and sufficient line weight |
| Gravure Printing | Detailed logos, smooth gradients, dense colors | High-volume cartons, paper wraps | Better for standardized artwork and long runs |
Enhance Packaging Logos With Decorative Finishes
Decorative finishes can add contrast, depth, or tactile emphasis to a packaging logo, but each finish places different limits on line weight, spacing, and detail. The logo artwork needs to match the physical behavior of the selected finish so that fine elements do not close up, break, or lose definition during production.
Foil Stamping

Foil stamping gives packaging logos a metallic, reflective, or specialty-color appearance that standard ink cannot reproduce. Gold and silver remain common choices, while colored, holographic, and matte foils allow the logo to take on different visual personalities without changing its basic shape.
Wordmarks, monograms, borders, and graphic symbols usually benefit most from the clean, solid foil surface. Because foil does not reproduce tonal shading in the same way as process printing, gradients and transparency normally need to be converted into solid areas. Choose foil stamping when the logo needs strong visual contrast or a metallic brand accent.
Embossing and Debossing

Embossing and debossing turn the packaging logo into part of the physical structure of the box surface. Embossing raises the mark above the paper, while debossing presses it inward, creating recognition through light, shadow, and touch rather than color alone.
Logos built around strong typography, initials, seals, or simple symbols respond especially well to this treatment. Ink or foil can be added, but a blind embossed or debossed logo also creates a restrained tone-on-tone effect. This makes the finish especially suitable for brands that want tactile depth without relying on bright color or reflective shine.
UV Printing

UV printing gives packaging logos a high-gloss or raised surface that contrasts with the surrounding material. Spot UV increases light reflection over selected areas, while raised UV adds more visible thickness and tactile definition.
A printed logo can retain its original color underneath the UV layer, making the finish useful when you want emphasis without replacing the existing artwork with foil or embossing. A separate mask layer defines the exact coating area. The added gloss or relief can make an existing printed logo more prominent without changing its underlying color design.
Textured Varnish
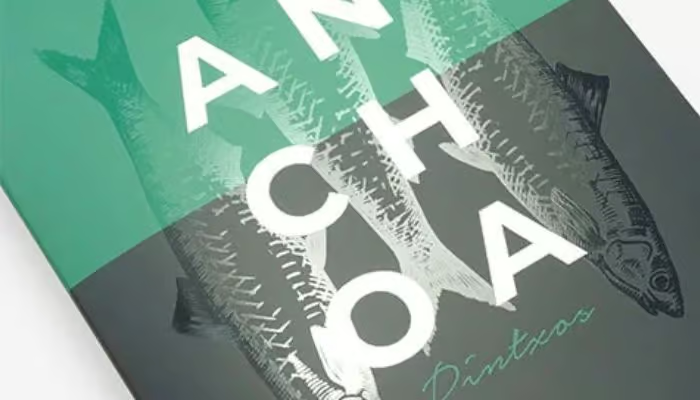
Textured varnish changes the feel of the logo rather than making it highly reflective or deeply embossed. Depending on the formulation, the treated area can feel grainy, matte, rough, or otherwise distinct from the surrounding surface.
Larger wordmarks and graphic marks usually show the tactile effect more clearly because they provide enough surface area for the texture to register by touch. The finish suits branding that calls for a quieter sensory detail rather than metallic shine or pronounced relief. When subtle tactile branding matters more than shine, textured varnish creates distinction through touch rather than obvious visual effects.
Prepare Print-Ready Logo Files for Packaging Box Printing

Print-ready logo files preserve the exact shapes, colors, and production layers required for box printing. Clean artwork also prevents font substitution, missing links, low-resolution graphics, and incorrect finishing layers from changing the logo during prepress or production.
- Use vector artwork: Supply AI, EPS, or editable PDF files for logos whenever possible. Vector graphics stay sharp at different print sizes and make color separation easier.
- Set raster elements to 300 DPI: Any bitmap image used in the logo should be at least 300 DPI at its final printed size. Enlarging a low-resolution image does not restore missing detail.
- Outline the fonts: Convert logo typography to outlines before final submission so the letterforms do not change when the original font is unavailable.
- Embed linked graphics: Include or embed every placed image and graphic asset so no elements disappear when the artwork moves between systems.
- Define production colors clearly: Set CMYK values or Pantone references in the final file instead of leaving critical brand colors in RGB.
- Separate special finishes: Create dedicated artwork layers or spot-color masks for foil stamping, embossing, debossing, UV effects, or textured varnish. Clear layer names help prevent decorative areas from being interpreted as ordinary print graphics.
- Remove unnecessary artwork: Delete hidden objects, duplicate logo versions, unused color swatches, and stray elements that can create confusion during prepress.
Maintain Packaging Logo Consistency Across Different Box SKUs
Consistent packaging does not require every box to use the logo at the same size or position. The goal is to preserve the same brand rules across different structures, materials, and dimensions so each SKU still looks like part of one packaging system.

Master Logo Specifications
A master logo specification gives every packaging SKU the same starting point. It defines the approved logo artwork, proportions, clear space, minimum size, orientation, and permitted color versions before individual box layouts are developed.
Use one controlled source file rather than allowing each SKU to recreate or redraw the logo. This reduces small differences in spacing, letterforms, symbol proportions, or alignment that can become noticeable when several packages appear together.
Brand Color References
Brand color references turn a visual color choice into a repeatable production target. Record the approved Pantone code, CMYK values, or other production references used for the logo, then link those references to the relevant substrate and printing method.
A single color value does not always look identical on coated paper, kraft, or textured stock. For critical brand colors, retain an approved printed sample or physical color reference alongside the digital specification so future SKUs and repeat orders can match the intended result more closely.
Approved Logo Variations
Different box formats may require more than one logo configuration. A horizontal wordmark may suit a wide lid, while a stacked version or compact symbol may fit a narrow drawer front or small folding carton more effectively.
Define these variations as part of the brand system rather than modifying the logo case by case. Each version can follow fixed proportions, color rules, and minimum-size limits to maintain recognition across the packaging range.
Artwork Version Control
Version control prevents outdated logo files from entering production. Clear file names, revision numbers, and dated artwork records make it easier to identify the current version and remove obsolete files from active projects.
This becomes especially important for multi-SKU ranges, regional editions, seasonal updates, and repeat orders. A controlled artwork record helps keep logo files, color references, and finishing instructions consistent from one production run to the next.
Check Packaging Logo Printing Before Mass Production
Pre-production checks confirm that the packaging logo can move from artwork to the finished box without losing clarity, color accuracy, placement, or finishing detail. Review the digital file first, then verify the logo on a physical sample before releasing the design for mass production.

Artwork and Dieline Review
Start with the final production artwork and confirm that every logo element matches the correct packaging dieline. Check the logo version, dimensions, orientation, color settings, finishing layers, and relationship to cut lines, folds, openings, and structural panels.
This review helps catch errors before mass production. An outdated dieline can shift the logo after cutting, a missing foil or UV layer can remove part of the finish, and an old logo file can create inconsistencies across SKUs. A clean dieline and controlled artwork file reduce the risk of misplacement, missing elements, and costly rework.
Logo Clarity and Fine Details
Review the logo at its actual production size to confirm that small text, thin strokes, counters, spacing, and graphic edges remain clear after printing or finishing. An enlarged screen view can hide problems that only appear once the artwork is reduced to its final size.
Fine details may disappear, merge, or fill in when line weights are too light, or gaps are too narrow. Textured paper, heavy ink coverage, and some finishing processes can also reduce definition. A physical sample reveals these issues before they carry into mass production.
Color and Finish Verification
Compare the printed logo against the defined CMYK, Pantone, foil, or varnish reference under consistent lighting. Pay attention to color shifts, uneven ink density, weak opacity on dark paper, foil gaps, incomplete embossing, or UV areas that extend beyond the logo boundary.
These defects can make the same logo look different from the artwork or from one SKU to another. Paper tone, surface texture, registration, pressure, and coating thickness can all affect the result, so color and finish verification confirms that the final logo matches the intended brand appearance before mass production begins.
Placement and Alignment
Confirm that the logo sits in the intended position on the assembled box, not just on the flat artwork. Compare its distance from panel edges, centerlines, openings, seams, and nearby design elements to make sure the visual balance remains consistent after cutting, folding, wrapping, and assembly.
Misalignment can make a centered logo look uneven, push the mark too close to an edge, or shift paired elements out of line across panels. Evaluating placement on the finished sample helps catch these structural errors before they repeat across the full production run.
Physical Packaging Sample Evaluation
Examine the completed packaging sample as a whole rather than reviewing each logo detail in isolation. The sample shows whether the logo, material, print method, finish, box structure, and surrounding graphics work together as intended in the final physical format.
Look for issues that digital proofs may not reveal, such as weak contrast on the selected paper, uneven foil transfer, loss of detail on textured surfaces, or a logo that feels too small once the box is assembled. The physical sample provides the closest pre-production reference for deciding whether the logo is ready for mass production.
Reference Standards for Repeat Production
Use the final production sample, color references, logo artwork, and finishing specifications as the benchmark for future orders. These records give each repeat run a clear target for logo color, placement, foil tone, embossing depth, varnish area, and other visible details.
Without a fixed reference, small differences can accumulate between batches, especially when paper lots, ink mixing, press settings, or finishing conditions change. A documented production standard helps keep the packaging logo visually consistent across repeat orders and multiple box SKUs.
Work With Gentlever for Reliable Packaging Logo Printing
Gentlever supports packaging logo projects from artwork review through sampling and mass production. We help you match the logo design with the box structure, paper surface, color system, printing method, and decorative finish so the final result stays clear and consistent on the finished packaging.
Before production, we can review dielines, logo files, Pantone or CMYK references, foil and UV layers, and other print details that affect reproduction. Sampling also gives you a physical reference for color, placement, clarity, and finishing effects before the bulk order moves forward.
Conclusion
A clear and consistent packaging logo depends on more than visual design. File quality, color control, material choice, print method, finishing, size, placement, and pre-production checks all influence how the logo appears on the finished box.
Designing a packaging logo with production limits in mind helps protect brand consistency across different box formats and repeat orders. If you need support with logo artwork, printing methods, finishes, or custom box production, contact us at Gentlever to discuss your packaging requirements.